Press Brake Tooling for Common Straight-Line Bending
Product Introduction
Shengpu Tooling manufactures standard straight punch and double V die sets for common sheet metal bending applications.
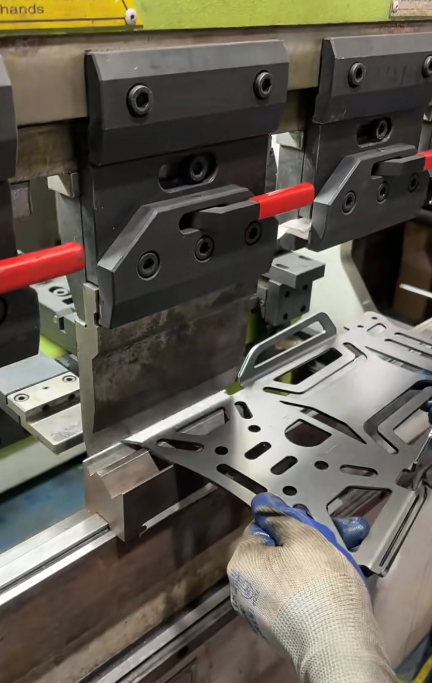
A standard straight punch applies bending force vertically along the center line, while a double V die, also called a 2V die, allows operators to switch between two V openings by simply turning the die over. This combination is widely used in sheet metal workshops because it can cover several common material thicknesses with fewer tooling changes.
For small-batch and multi-size production, a standard straight punch with a double V die is a practical press brake tooling solution for reducing setup time, lowering tooling cost, and improving daily bending efficiency.
Core Product Capabilities
- Straight punch rigidity: Center-line load design helps keep vertical bending stable and reduces side loading during normal straight-line bending.
- Double V die efficiency: One lower die includes two V openings, such as V10 + V16, allowing quick switching by flipping the die.
- Matched to common sheet thickness: Suitable for common workshop materials such as 1.0 mm, 1.5 mm, 2.0 mm, and 3.0 mm sheets.
- Tool steel and heat treatment: Available in 42CrMo forged steel, Cr12MoV, and other tool steels, with through hardening around HRC47±2.
- Precision grinding: Precision ground working surfaces help maintain stable bending angles and smooth tooling contact.
- Custom machine fit: Clamping interface, V opening size, tool length, and segmented tooling can be customized according to your press brake model.
Common V Opening Reference
- 1.0 mm sheet: V6–V8, approximate inside radius 1.0–1.3 mm, minimum flange about 5 mm
- 1.5 mm sheet: V10–V12, approximate inside radius 1.7–2.0 mm, minimum flange about 7 mm
- 2.0 mm sheet: V16, approximate inside radius 2.7 mm, minimum flange about 11 mm
- 3.0 mm sheet: V24, approximate inside radius 4.0 mm, minimum flange about 17 mm
Note: The above reference is mainly for low carbon steel air bending. Stainless steel and high-strength steel usually require a wider V opening, while aluminum may use a smaller V opening depending on the material condition and surface requirements.
Selection and Use Tips
- Match the double V die to your main sheet thicknesses. Choose two V openings based on the materials you bend most often.
- Check alignment after flipping the die. Clean chips and dust before use, then check whether the punch tip aligns with the V groove center.
- Start with the 8T rule. For example, a 2 mm sheet can start with a V16 press brake V die, then adjust according to material and bending results.
- Check tonnage and minimum flange length. A smaller V opening is not always better; it may increase tonnage and surface marks.
- Replace or regrind damaged punch tips. A chipped punch edge can directly affect surface quality and bending accuracy.
Why Choose Shengpu Tooling
Shengpu Tooling focuses on custom press brake tooling for sheet metal bending. We manufacture standard straight punches, double V dies, 2V dies, press brake V dies, upper punches, lower dies, hemming dies, radius dies, offset dies, gooseneck punches, and special-shaped tooling.
Our team can help customers choose the proper V die opening, punch tip radius, tooling length, and clamping system according to drawings, material thickness, bending angle, and machine model.
Get a Custom Solution
If your current press brake tooling causes unstable angles, surface marks, short flange support problems, or high tonnage, send us your drawing and bending parameters.
Shengpu Tooling will help review your production requirements and provide a suitable standard straight punch and double V die solution.
Contact Shengpu Tooling
WhatsApp Business: +86 15155556086
Email: leah@sinobend.com
Website: shengputooling.com