How to Choose the Right 30° Acute-Angle Press Brake Tooling for Your Machine
1. What Is Acute-Angle Press Brake Tooling?
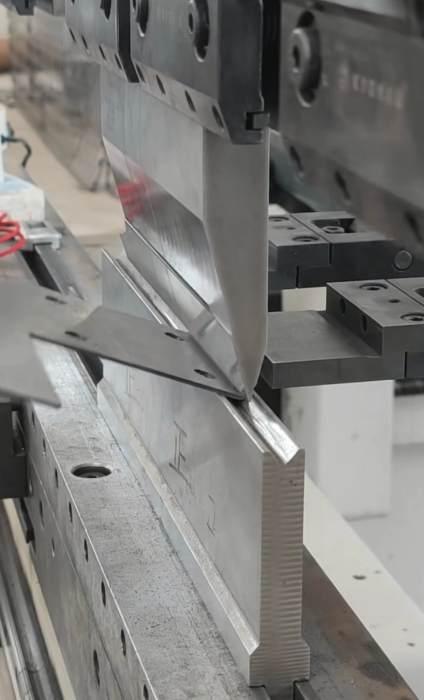
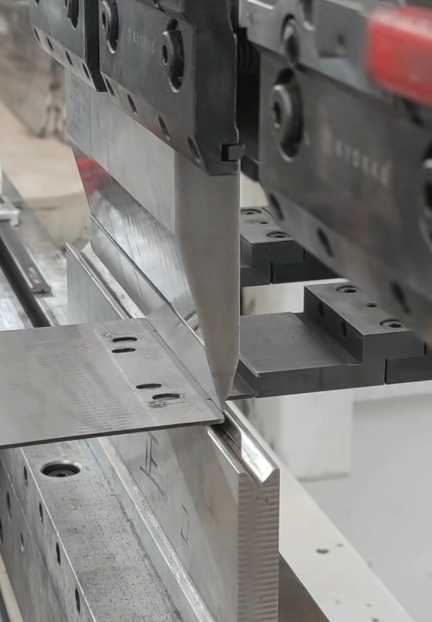
Acute-angle press brake tooling is a set of upper and lower tools designed to form bend angles smaller than 90°. Common acute tooling angles include 30°, 28° and 35°. Smaller angles may also be used for special applications.
An acute-angle tooling set generally includes two main components:
- Upper punch: Installed on the press brake ram or upper beam. It presses the sheet into the lower die.
- Lower die: Also called lower tooling, bottom tooling or a V-die. It is installed on the press brake bed and supports the sheet during bending.
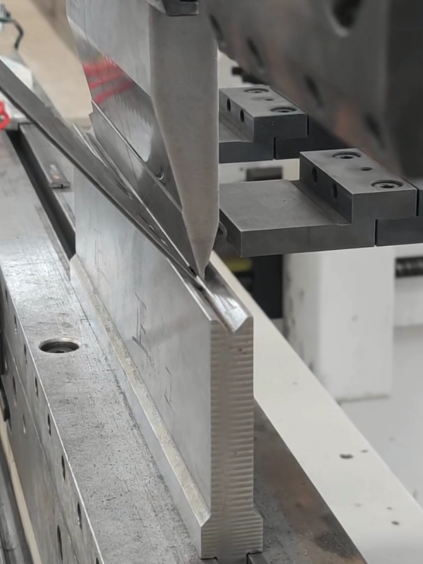
Because acute-angle tooling has a narrow and pointed profile, it provides additional clearance for the workpiece. This helps reduce interference between the flange and the tooling during acute bending, pre-hemming, narrow-channel forming and short return-flange applications.
2. What Is 30° Press Brake Tooling Used For?
30° tooling is not only used to produce a finished 30° angle. It is mainly used for the following applications.
Acute-Angle Bending
30° punches and dies can form angles smaller than 90° for parts that require angled edges, sharp bends or special interlocking structures.
Pre-Hemming
Hemming is normally completed in two stages:
- Use 30° acute-angle tooling to pre-bend the sheet edge.
- Use a flattening punch or hemming tool to close the pre-bent section.
Therefore, 30° tooling is commonly used during the first stage of hemming.
Narrow Channels and Short Return Flanges
For narrow channels, U-shaped parts and Z-shaped parts, standard 88° or 90° tooling may interfere with the workpiece. The narrow profile of acute-angle tooling provides additional clearance.
Springback Compensation
Stainless steel, high-strength steel and certain aluminum alloys may produce significant springback. Acute-angle tooling allows the operator to overbend the material so that it returns to the target angle after unloading.
Typical Applications
30° tooling is often used for:
- Electrical enclosures
- Ductwork
- Brackets
- Elevator panels
- Furniture components
- Metal doors
- Narrow frames
- Return-flange components
3. Difference Between a 30° Upper Punch and a 30° Lower Die
| Item | 30° Upper Punch | 30° Lower Die |
|---|---|---|
| Installation position | Press brake ram or upper beam | Press brake bed or lower beam |
| Main function | Presses the sheet downward and forms the inside angle | Supports the sheet and determines the V-die geometry |
| Key parameters | Tip angle, tip radius, height and length | V-opening, die angle, shoulder radius and die height |
| Main wear areas | Punch tip and tip radius | Die shoulders and V-groove |
| Common styles | Straight punch, gooseneck punch and special forming punch | Single-V, double-V and multi-V dies |
| Main influence | Inside radius, bending depth and clearance | Bend angle, sheet support and bending force |
Angle-Matching Principle
The upper punch and lower die must be compatible. In general, the punch angle should not be greater than the working angle of the lower die.
For example:
- A 30° lower die can be used with a 30° upper punch.
- A slightly sharper punch, such as a 28° punch, may also be suitable in some applications.
- A 30° lower die should not be paired with an 88° or 90° punch without confirming compatibility.
The tooling load rating, tip radius, V-opening, clamping system and press brake model must also be checked before use.
4. When Should You Use Acute-Angle Tooling?
88° or 90° tooling is suitable for general 90° bending. It generally offers good rigidity, higher load capacity and lower cost.
Consider acute-angle tooling when:
- The finished bend angle is less than 90°.
- The part requires hemming or pre-hemming.
- The material has significant springback.
- The return flange or channel wall may interfere with a standard punch.
- The part includes narrow channels, short flanges or deep box sections.
- Several bending angles are required using the same tooling setup.
- Additional clearance is needed for a pre-hemming operation.
Many manufacturers use 88° or 90° tooling for standard production and keep a separate 30° tooling set for special parts and hemming applications.
5. How to Choose CNC Press Brake Lower Tooling
1. Select the Correct V-Opening
The V-opening is one of the most important lower-die parameters. As a starting point, the V-opening is often selected based on the material thickness.
General guidelines include:
- Thin sheet: approximately 6–8 times the material thickness
- Mild steel: approximately 8 times the material thickness
- Stainless steel or high-strength steel: approximately 10–12 times the material thickness
- Aluminum: approximately 5–6 times the material thickness
These are only initial guidelines. The final selection should also consider material strength, bend angle, inside radius and machine capacity.
An excessively narrow V-opening may cause:
- Increased bending force
- Surface marks
- Material cracking
- Die shoulder damage
- Press brake overload
2. Select the Die Angle
A 30° lower die is commonly selected for acute-angle bending. Hemming normally requires two separate operations:
- A 30° acute-angle die for pre-bending
- A flattening or hemming die for final closing
The pre-bending die and flattening die should not be treated as the same tool.
3. Select the Shoulder Radius
The lower-die shoulder radius affects the sheet surface quality and bending radius.
A shoulder radius that is too small may cause:
- Surface dents
- Coating damage
- Cracking
- Inconsistent bend radius
Special attention should be given to shoulder radius when processing stainless steel, aluminum, coated sheet and polished sheet.
4. Match the Tooling to the Material Thickness
Material thickness affects:
- V-opening
- Inside radius
- Required bending force
- Minimum flange length
- Tool load capacity
Thick plate should not be forced into an excessively narrow V-opening or a very small inside radius, as this may overload the machine and tooling.
5. Calculate the Required Bending Force
A narrow V-opening, thick material, high-strength steel and stainless steel can all increase the required bending force.
Before ordering tooling, confirm:
- Press brake rated tonnage
- Maximum tooling load
- Permitted load per meter
- Localized or concentrated load limits
6. Check Machine Compatibility
Before ordering CNC press brake lower tooling, confirm:
- American, Promecam, New Standard or European-style clamping
- Wila, Amada or other proprietary interfaces
- Lower-die height
- Shut height
- Working length
- Segmentation options
- Press brake bed design
- Backgauge travel
- Crowning or deflection-compensation range
Gooseneck punches, segmented tooling and special-height lower dies may change the available opening height of the press brake.
6. How Acute Tooling Helps Control Springback
Springback occurs when the sheet partially returns to its original shape after the punch is raised.
The following values are only general references:
| Material | Approximate Springback |
|---|---|
| Mild steel | 1°–3° |
| Aluminum | 2°–5° |
| Stainless steel | 3°–6° or more |
| High-strength steel | 4°–8° or more |
Acute-angle tooling provides additional bending-angle capacity, allowing the operator to overbend the material and compensate for springback.
For better consistency in production:
- Use a CNC press brake with angle measurement when possible.
- Record correction values for different materials and thicknesses.
- Keep material thickness and rolling direction consistent.
- Use the same V-opening throughout the production batch.
- Perform a test bend before starting production.
- Do not estimate springback for high-strength steel or stainless steel based only on experience.
7. Common Tooling Selection Mistakes
Using an Oversized V-Opening for a Short Flange
The sheet may not be supported properly, causing slipping, inconsistent angles or positioning errors.
Ignoring the Tool Load Rating
Acute tooling should not automatically be used at the same load as standard 88° or 90° tooling. Always confirm the manufacturer’s load data.
Mismatching the Upper and Lower Tool Angles
If the punch angle is larger than the lower-die angle, the punch may not enter the V-groove correctly and tooling interference may occur.
Using an Extremely Narrow V-Opening for Thick Plate
This can increase the bending force and lead to cracking, tool deformation or press brake overload.
Ignoring Material Springback
If springback is not considered, the finished part may not meet the required angle and production rework may be necessary.
Failing to Check the Machine Interface
An incorrect clamping system, tooling height or shut height may prevent the tooling from being installed correctly.
Using Standard Tooling on Coated or Polished Sheet
Sharp or rough die shoulders may damage the surface. Non-marking tooling or specially finished tooling may be required.
Ignoring Part Geometry
Deep boxes, narrow channels and complex return flanges may require a gooseneck punch, segmented tooling or custom tooling instead of a standard straight punch.
8. Frequently Asked Questions
What is 30° press brake tooling used for?
30° press brake tooling is used for acute-angle bending, pre-hemming, narrow channels, short return flanges and springback compensation.
What is acute-angle tooling on a press brake?
Acute-angle tooling is a set of upper and lower press brake tools with a working angle below 90°. Common examples include 30°, 28° and 35° tooling.
What is CNC press brake bottom tooling?
CNC press brake bottom tooling refers to the lower tooling installed on the press brake bed. It is also called a lower die or V-die. Its V-opening, angle and shoulder radius affect the final bending result.
What is the difference between a press brake upper punch and lower die?
The upper punch presses the sheet and forms the inside radius. The lower die supports the sheet and determines the bending geometry through its V-opening and profile.
Can a 30° lower die be used for hemming?
Yes. A 30° lower die is commonly used for the first pre-bending stage of hemming. A flattening or hemming tool is then used to close the edge.
How do acute-angle tools affect springback?
They provide additional angular clearance for overbending, helping compensate for springback so that the part reaches the correct final angle after unloading.
What information is needed to order custom press brake tooling?
You should provide:
- Press brake brand and model
- Clamping system
- Material type
- Sheet thickness
- Required bend angle
- Flange length
- Target inside radius
- Tooling length
- Segmentation requirements
- Part drawing or sample
9. Need 30° Acute-Angle Tooling or CNC Press Brake Lower Tooling?
We supply used press brakes, shearing machines and matching press brake tooling, including:
- 30° acute-angle upper punches
- 30° acute-angle lower dies
- Single-V lower dies
- CNC press brake lower tooling
- Hemming tooling
- Gooseneck punches
- Segmented press brake tooling
- Custom press brake tooling
Send us your press brake model, material thickness, required bend angle and part drawing. Our team can recommend suitable tooling and provide a quotation.
Send us your press brake model, material thickness, required bend angle and part drawing. We can recommend a suitable 30° upper punch, single-V lower die or custom CNC press brake tooling.
WhatsApp Business
With a pre-filled message:
Send Your Tooling Requirements
No responses yet